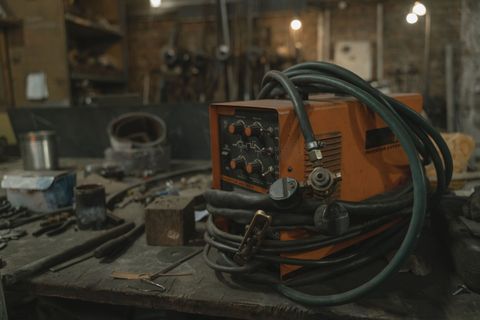
MIG Welding Machines: Explore Overview, Basics, Explanation, Knowledge, and Key Details
Metal Inert Gas (MIG) welding is a widely used arc-welding process in which an electric arc joins metal components using a continuously supplied consumable wire electrode. A shielding gas protects the molten weld area from atmospheric contamination. The process is also commonly known as Gas Metal Arc Welding (GMAW).
A MIG welding machine provides the electrical power, wire-feeding control, and operating settings required to create a stable welding arc. It is used in automotive manufacturing, fabrication, construction, machinery production, and metal component assembly.
Modern MIG welding equipment may include inverter power sources, digital displays, programmable settings, automatic wire feeders, and robotic integration. These features help operators control welding parameters and maintain consistent weld quality.
This guide explains MIG welding machine fundamentals, types, components, working principles, applications, modern technologies, Indian safety considerations, and best practices.
Understanding MIG Welding Machines
A MIG welding machine joins metal parts by creating an electric arc between a continuously fed wire electrode and the workpiece. The heat from the arc melts the wire and the edges of the base metal. The molten material forms a weld pool, which solidifies into a joint as the welding torch moves along the intended path.
Shielding gas flows through the welding torch and protects the arc and molten metal from oxygen, nitrogen, and other atmospheric contaminants.
Common shielding gases include:
Argon
Carbon dioxide
Argon and carbon dioxide mixtures
Other specialised gas mixtures selected for particular metals and welding conditions
MIG welding is generally associated with non-ferrous metals when inert shielding gases are used. In industrial practice, the broader GMAW process also includes active shielding gases, such as carbon dioxide or argon-based mixtures, and is often called Metal Active Gas (MAG) welding.
Typical materials joined using suitable GMAW processes include mild steel, stainless steel, and aluminium alloys. The wire, gas, polarity, and machine settings must be selected according to the material and joint requirements.
Importance of MIG Welding Machines
MIG welding machines are important in modern metal fabrication because they support continuous welding and can be adapted to a wide range of component sizes and production environments.
Continuous wire feeding: The consumable electrode is supplied automatically, reducing the need for frequent electrode replacement.
Versatile applications: Suitable configurations can join different metal types and thicknesses.
Adjustable parameters: Operators can control voltage, wire-feed speed, and other settings to suit the welding task.
Production consistency: Properly configured machines can produce repeatable welds.
Automation compatibility: MIG welding can be integrated with robotic arms, fixtures, and automated production systems.
Multiple welding positions: Depending on the process settings, wire type, and operator skill, MIG welding can be performed in several positions.
Main Types of MIG Welding Machines
MIG welding machines are classified by their power source, operating capacity, automation level, and intended application.
1. Standard MIG Welding Machine
A standard MIG welding machine is commonly used for general metal fabrication and repair work. It includes a power source, wire feeder, welding torch, and shielding-gas arrangement.
Typical features include:
Adjustable welding voltage
Controlled wire-feed speed
Compatibility with different wire diameters
Gas-flow adjustment
Support for common steel and aluminium welding configurations
2. Industrial MIG Welding Machine
An industrial MIG welding machine is designed for demanding production environments. It may have a higher duty cycle, stronger power output, advanced cooling, and more precise parameter control.
Common applications include structural fabrication, automotive components, machinery frames, and heavy metal assemblies.
3. Automatic MIG Welding Machine
An automatic MIG welding machine performs welding operations with reduced manual torch movement. It may use mechanised carriages, automated fixtures, programmable systems, or robotic arms.
Its main features can include:
Programmable welding sequences
Automatic wire feeding
Controlled torch movement
Consistent travel speed
Integrated safety interlocks
Production monitoring
4. Heavy Duty MIG Welding Machine
A heavy duty MIG welding machine is intended for applications involving thicker materials, higher current levels, and extended operating periods.
Depending on its design, it may include:
High-current output
Robust power electronics
Advanced cooling arrangements
Heavy-duty wire-feeding systems
Higher duty-cycle ratings
Support for larger welding wires
The actual operating capacity should be assessed using the machine's rated output and duty-cycle specifications.
5. Inverter MIG Welding Machine
An inverter MIG welding machine uses electronic inverter technology to convert and regulate electrical power. Inverter designs are generally more compact than traditional transformer-based power sources of comparable output.
Common characteristics include:
Electronic control of welding output
Adjustable voltage and current characteristics
Compact construction
Efficient power conversion
Digital parameter displays on selected models
Support for synergic or pulsed welding on advanced systems
6. CNC MIG Welding Machine
A CNC MIG welding machine uses computer-controlled movement to guide the welding torch along programmed paths. It can be integrated with fixtures, linear motion systems, or robotic equipment.
It is useful for repeated components that require controlled torch positioning, travel speed, and welding sequences.
Main Components of MIG Welding Equipment
MIG welding equipment consists of electrical, mechanical, gas-delivery, and wire-feeding systems.
Component | Main function |
|---|---|
Welding power source | Supplies controlled electrical power |
Wire feeder | Feeds the consumable electrode continuously |
Welding torch or gun | Directs the wire and shielding gas towards the joint |
Contact tip | Transfers welding current to the wire |
Gas nozzle | Directs shielding gas around the welding area |
Shielding-gas cylinder | Stores the selected shielding gas |
Gas regulator and flowmeter | Controls gas pressure and flow |
Welding wire spool | Holds the consumable electrode wire |
Work return clamp | Completes the electrical circuit through the workpiece |
Cooling system | Manages heat in water-cooled equipment |
Control panel | Allows adjustment of welding parameters |
Protective equipment | Helps protect the operator from welding hazards |
MIG Welding Machine Working Principle
MIG welding works through an electric arc formed between a continuously fed wire electrode and the base metal. The arc generates heat that melts the wire and the adjoining edges of the workpiece.
The shielding gas flows through the torch nozzle and protects the molten weld pool from atmospheric contamination. As the torch travels along the joint, the molten metal cools and forms a solid connection.
A typical operating sequence includes:
Selecting a suitable welding wire for the base material.
Choosing the correct shielding gas.
Connecting the power source, wire feeder, torch, and gas supply.
Preparing and cleaning the joint surfaces.
Setting voltage, wire-feed speed, gas flow, and other parameters.
Positioning the torch at the beginning of the joint.
Starting the wire feed and establishing the arc.
Moving the torch along the intended welding path.
Allowing the weld pool to solidify.
Inspecting the completed weld for defects and dimensional accuracy.
Correct setup is important because unsuitable parameters can cause porosity, spatter, incomplete fusion, burn-through, or irregular weld formation.
MIG Welding Transfer Modes
Metal transfer describes how molten electrode material moves from the wire into the weld pool. Different transfer modes are selected according to material thickness, welding position, shielding gas, and required weld characteristics.
Short-Circuit Transfer
In short-circuit transfer, the wire repeatedly touches the weld pool, creating a short circuit that transfers molten metal. It is commonly used for thinner materials and applications where lower heat input is required.
Globular Transfer
Globular transfer involves larger droplets of molten metal moving from the wire towards the weld pool. It is generally associated with higher spatter and is used in particular material and gas combinations.
Spray Transfer
Spray transfer produces a stream of smaller droplets moving across the arc. It generally requires higher current levels and suitable shielding-gas mixtures. It is commonly used for thicker materials and suitable welding positions.
Pulsed Spray Transfer
Pulsed MIG welding alternates between higher peak current and lower background current. This helps control metal transfer and heat input, making it useful for selected thin materials, aluminium, and position-sensitive applications.
Applications of MIG Welding Machines
MIG welding machines are used in several industries because the process supports continuous electrode feeding and a wide range of material configurations.
Industry | Typical applications |
|---|---|
Automotive | Vehicle frames, body structures, and component assemblies |
Construction | Structural steel and metal framework fabrication |
Heavy engineering | Industrial frames, equipment housings, and large assemblies |
Shipbuilding | Selected steel and aluminium structural joints |
Agriculture | Equipment frames, trailers, and metal components |
Railway manufacturing | Selected structural and fabricated assemblies |
Furniture manufacturing | Metal frames, supports, and tubular components |
General fabrication | Brackets, enclosures, panels, and metal structures |
Recent Developments and Industry Trends
MIG welding technology continues to develop through improvements in inverter electronics, digital controls, automation, and weld monitoring.
Synergic Welding Controls
Synergic MIG systems coordinate welding voltage and wire-feed speed using programmed relationships. Operators select a material, wire diameter, and gas combination, and the system recommends suitable parameters. Fine adjustments may still be necessary for the actual joint and welding conditions.
Pulsed MIG Technology
Pulsed MIG systems regulate current in alternating peak and background phases. This can help control droplet transfer and heat input, particularly when welding aluminium, stainless steel, and thinner materials.
Robotic MIG Welding
Robotic welding systems combine MIG power sources with programmable robotic arms, fixtures, sensors, and safety enclosures. They are used for repeated weld paths in automotive, machinery, and metal fabrication production.
Digital Monitoring and Data Recording
Advanced welding systems can record parameters such as current, voltage, wire-feed speed, and arc-on time. Some systems also support production monitoring and traceability through connected control platforms.
Improved Inverter Power Sources
Modern inverter designs use electronic switching and control systems to regulate welding output. They can provide compact machine designs and support advanced features such as pulse modes, synergic programs, and controlled arc characteristics.
Greater Attention to Welding Fume Control
Welding fume management remains an important part of workplace safety. Local exhaust ventilation, suitable extraction equipment, correct positioning, and exposure assessment are important, particularly in enclosed or poorly ventilated work areas.
Laws, Policies, and Standards in India
MIG welding operations in India should follow applicable workplace safety, electrical safety, fire prevention, and industrial standards. Requirements depend on the establishment, welding process, materials, and equipment configuration.
Occupational Safety, Health and Working Conditions Code, 2020
India's Occupational Safety, Health and Working Conditions Code, 2020 came into force on November 21, 2025, through Ministry of Labour and Employment notification S.O. 5321(E). The Code establishes a framework for occupational safety, health, and working conditions in covered establishments.
For MIG welding operations, important workplace precautions include:
Providing appropriate ventilation and welding-fume extraction.
Maintaining safe electrical connections and equipment.
Training workers in welding hazards and operating procedures.
Providing suitable eye, face, hand, and body protection.
Maintaining fire-prevention arrangements.
Establishing safe procedures for gas-cylinder storage and handling.
Keeping welding areas clear of unnecessary combustible materials.
BIS Standards for Arc Welding Equipment
The Bureau of Indian Standards publishes standards covering the construction, performance, testing, and safety of electric welding equipment.
One relevant standard is IS 16593 (Part 1):2021, based on IEC 60974-1:2017, which addresses arc-welding equipment and welding power sources. BIS also lists related parts covering areas such as liquid-cooling systems, arc-striking devices, and wire feeders.
The applicable standard should be checked against the equipment type and its intended use. A reference to a standard does not by itself establish that every machine requires the same certification arrangement.
ISO 4063:2023
ISO 4063:2023 establishes a standardised nomenclature and reference-number system for welding, brazing, soldering, and cutting processes. It supports consistent identification of welding processes in technical drawings, documentation, and welding procedure specifications.
Welding Procedure and Quality Requirements
Industrial welding projects may require documented welding procedures, qualified operators, inspection plans, and records of welding parameters. Requirements depend on the industry, engineering specification, applicable product standard, and contract or project documentation.
Fire and Electrical Safety
MIG welding produces heat, sparks, and intense arc radiation. Workplaces should use suitable electrical protection, cable inspection, safe earthing arrangements, fire-resistant screens, and appropriate fire-protection equipment. Gas cylinders should be secured, protected from heat, and handled according to relevant safety instructions.
Best Practices for Operating MIG Welding Machines
Correct machine setup and consistent operating practices help improve weld quality and reduce avoidable hazards.
Choose the correct wire: Match the electrode wire classification and diameter to the base metal and joint requirements.
Select suitable shielding gas: Use a gas or gas mixture appropriate for the material and transfer mode.
Prepare the joint: Remove oil, paint, rust, moisture, and other contaminants where required.
Check wire feeding: Inspect the drive rolls, liner, contact tip, and wire spool for correct alignment and condition.
Set suitable parameters: Adjust voltage, wire-feed speed, travel speed, and gas flow according to the welding procedure.
Maintain correct torch position: Use an appropriate torch angle, contact-tip-to-work distance, and travel direction.
Inspect gas delivery: Check hoses, regulators, connections, and flow settings for leaks or restrictions.
Monitor weld appearance: Look for porosity, excessive spatter, undercut, cracks, and incomplete fusion.
Maintain the equipment: Clean the torch, replace worn contact tips, inspect cables, and follow the manufacturer's maintenance schedule.
Control welding fumes: Use local exhaust ventilation and avoid positioning the head directly in the fume plume.
Protect the surrounding area: Use welding screens and remove or shield combustible materials.
Keep records: Record inspection results, maintenance, consumable details, and approved parameter settings.
Tools and Resources for MIG Welding
Technical tools and reference materials help with welding preparation, parameter selection, inspection, and equipment maintenance.
Tool or resource | Purpose |
|---|---|
Welding parameter charts | Help identify starting voltage and wire-feed settings |
Welding procedure specifications (WPS) | Document approved welding parameters and techniques |
Welding calculators | Assist with estimating electrical and welding parameters |
CAD software | Prepare component drawings and joint layouts |
Welding inspection gauges | Check weld dimensions and profiles |
Digital multimeter | Check electrical conditions where appropriate |
Gas flowmeter | Monitor shielding-gas flow |
Wire-feed speed meter | Verify electrode feeding speed |
Fume extraction equipment | Remove welding fumes from the working area |
BIS standards catalogue | Identify relevant Indian equipment standards |
ISO standards catalogue | Refer to international welding process classifications |
Frequently Asked Questions
1. What is a MIG welding machine?
A MIG welding machine uses an electric arc and a continuously fed consumable wire electrode to join metal components. Shielding gas protects the weld pool from atmospheric contamination.
2. What materials can MIG welding machines join?
Depending on the wire, shielding gas, and machine configuration, MIG welding can join mild steel, stainless steel, and aluminium alloys. Material preparation and welding parameters must be selected appropriately.
3. What is the difference between an inverter MIG welding machine and a conventional MIG machine?
An inverter MIG welding machine uses electronic power conversion and control to regulate welding output. Conventional transformer-based machines use a different power-conversion arrangement and are often larger and heavier for comparable output ratings.
4. What is a heavy duty MIG welding machine used for?
A heavy duty MIG welding machine is used for demanding fabrication involving thicker materials, higher current levels, and longer operating periods. Its suitability depends on rated output, duty cycle, wire-feeding capacity, and cooling arrangements.
5. What is the difference between MIG and TIG welding?
MIG welding uses a continuously fed consumable wire electrode. TIG welding uses a non-consumable tungsten electrode, with filler material added separately when required. MIG is commonly used for continuous production welding, while TIG is often selected for applications requiring precise control of the weld pool.
Conclusion
MIG welding machines are important equipment in metal fabrication and industrial manufacturing. They use a continuously fed wire electrode, an electric arc, and shielding gas to create metal joints. Different configurations, including industrial MIG welding machines, automatic MIG welding machines, heavy duty MIG welding machines, inverter systems, and CNC-controlled equipment, support a wide range of production requirements.
Developments in synergic controls, pulsed welding, robotic integration, inverter electronics, and digital monitoring continue to expand the capabilities of MIG welding equipment. Understanding machine components, wire selection, shielding gases, transfer modes, operating parameters, and safety practices helps maintain consistent welding quality.
Disclaimer: This article is intended for general informational and educational purposes only. Welding procedures, equipment specifications, safety practices, and regulatory requirements should be verified with qualified welding professionals and relevant authorities before practical application. No particular machine, product, brand, or organisation is guaranteed or endorsed.
Related Post...
CO2 Laser Cutting Machines: Explore Overview, Basics, Explanation, Knowledge, and Key Details
Updated: November 17, 2026
Read More
Gear Shaping Machines: Complete Guide to Basics, Technologies, Processes, Facts, and Best Practices
Updated: November 17, 2026
Read More
Mineral Water Filling Machines: Explore Overview, Basics, Explanation, Knowledge, and Key Details
Updated: November 16, 2026
Read More